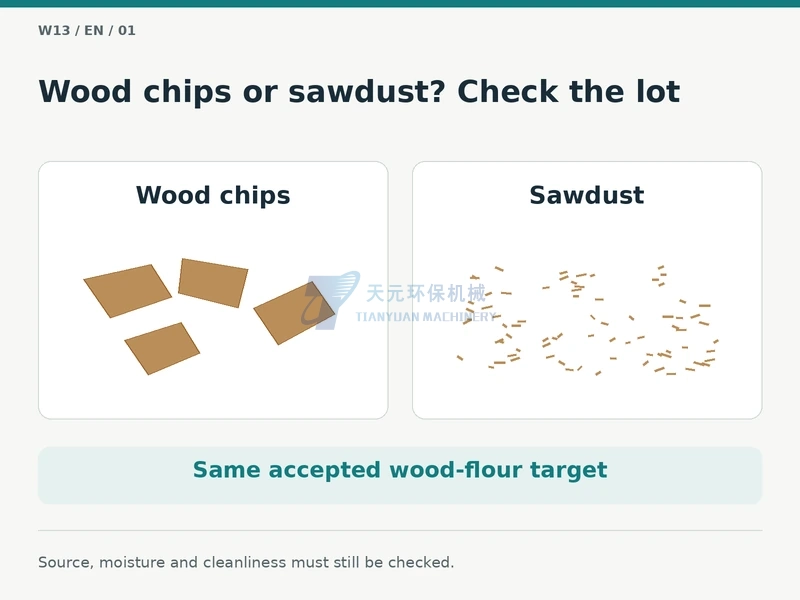
Both wood chips and sawdust can be candidates for wood flour production. The useful comparison is between the actual lots delivered to a plant: their source, dimensions, moisture, contamination and preparation needs. A smaller-looking raw material is not automatically a cleaner, cheaper or more consistent feed.
Key conclusion: Prefer the feedstock that can reliably reach the agreed wood-flour specification at the lowest verified total cost per accepted dry product. Suitable sawdust may avoid a coarse-reduction step; controlled wood chips may be preferable when their source and quality are more consistent. Neither category is automatically the winner.
Contents
Compare named lots, not just “chips” and “sawdust”
Wood chips are pieces produced by chipping or similar cutting; sawdust is particulate material from sawing. Neither name specifies a maximum dimension, moisture level, wood species or purity. Sawdust is also not automatically finished wood flour, and planer shavings should not be silently treated as identical sawdust.
Ask where the material was generated, whether species are mixed, whether bark is included and how it was stored. Clemons’s Wood Flour chapter connects raw-material selection with known species and freedom from bark, dirt and foreign matter. The purchasing question is therefore material identity and condition, not merely its commercial label.
Check the differences that can change preparation
The table is a conditional comparison, not a grading standard. Replace each general observation with a measurement or supply record from the proposed lot.
| Decision factor | Wood chips | Sawdust |
|---|---|---|
| Dimensions and form | Check thickness, length and oversize; additional reduction may be needed | Check coarse pieces, fibre bundles and the full size range |
| Moisture | Can be wet or conditioned; measure the actual lot | Can also be wet, uneven or moisture-regained |
| Source and contamination | Traceable cutting stock can help source control; not a purity guarantee | Single-source sawmill residues may be consistent; mixed collection needs review |
| Preparation | Reduce oversized material; condition only as required | May bypass coarse reduction only when the feed condition is already suitable |
| Receiving and feeding | Measure bulk density and actual delivery behavior | Do not assume a volumetric setting gives the same mass flow |
| Economic comparison | Include preparation and rejected material | Include screening, drying or cleaning that is actually necessary |
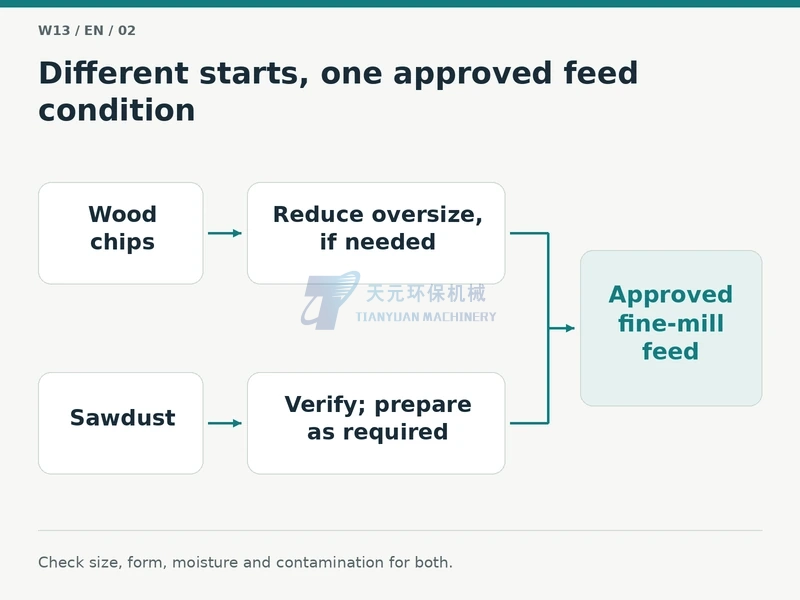
Both routes must reach the same approved mill-entry condition
For chips, first check whether the real dimensions and form meet the chosen fine mill’s limit. Oversized chips require suitable upstream reduction. That preparation is not the same task as final wood-flour grinding.
For sawdust, check before declaring that preparation is unnecessary. Large fragments, unsuitable moisture or foreign matter may still require screening, cleaning, conditioning or size reduction. Avoid grinding already-suitable feed again merely to reproduce a standard-looking line diagram.
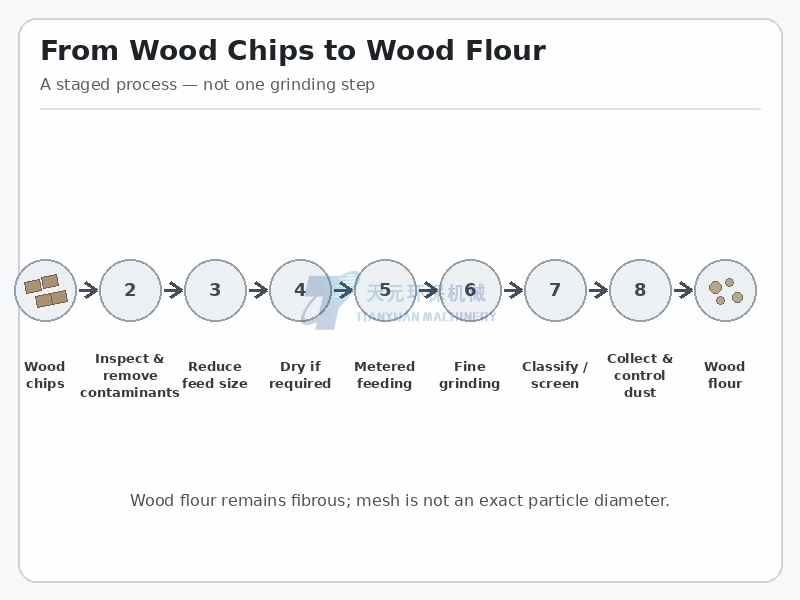
The two routes should converge on a defined, approved fine-mill feed condition. For the complete chips-to-product route, use the existing wood chips to wood flour process guide; this comparison is about choosing and preparing feedstock, not creating another page for that full process.
Do not pay for water without knowing the basis
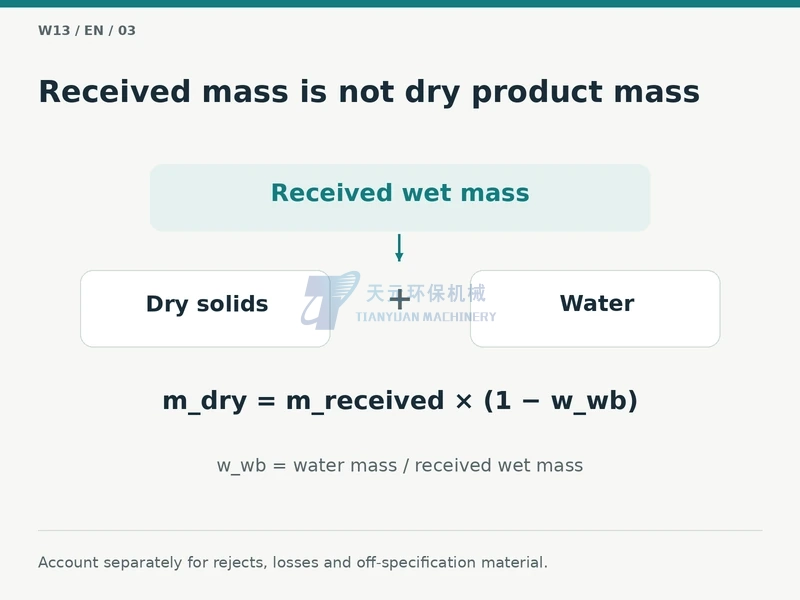
Compare moisture measurements made on a consistent basis. On a wet basis, received mass contains dry wood solids plus water; on a dry basis the percentage uses dry solids as its denominator. Confirm the basis rather than interpreting an unexplained percentage.
For accounting only: dry-solid mass = received wet mass × (1 − wet-basis moisture fraction). This identity is not a recommended moisture target, and it does not equal accepted wood-flour output. Rejected contaminants, process losses and off-specification fractions still need separate accounting.
The wood moisture guide explains the measurement distinction. A supplier’s “dry sawdust” or “fresh chips” label cannot replace representative sampling, preservation and the agreed test method.
Compare total cost per accepted dry product
A low purchase price per delivered tonne can be offset by preparation, drying, handling, rejected material or a lower accepted yield. Conversely, a more expensive but consistent supply may reduce preparation burden. Neither outcome can be assumed without site-specific costs and a comparable product target.
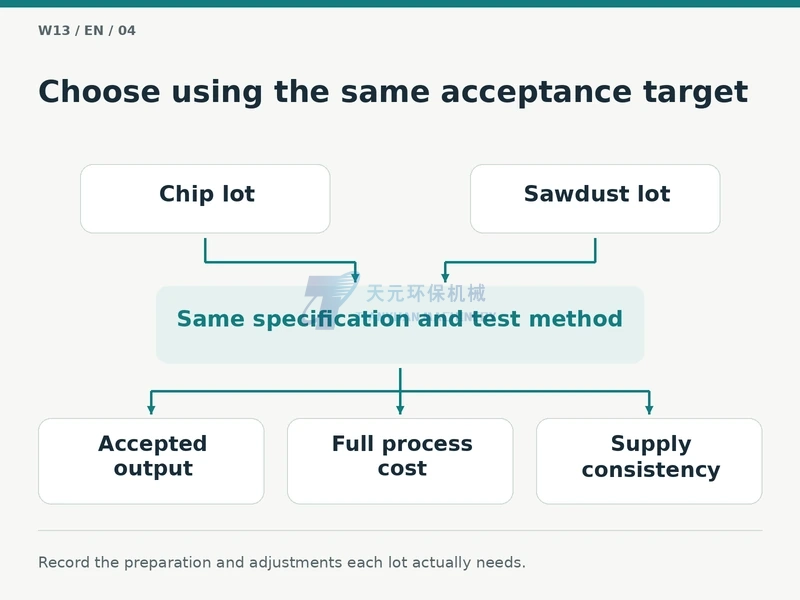
Use a common accounting boundary: delivered feed cost plus non-overlapping preparation, drying, milling, separation/collection and waste-handling costs, divided by accepted-product dry mass. State which costs are included. Avoid double-counting electricity already included in a stage charge.
Evaluate supply continuity, lot changes and storage alongside cost. Record what happens when the supplier changes species or collection source. Do not silently blend a new lot and treat the previous trial as proof that it is equivalent.
Run a fair comparison using the same acceptance target
Compare representative samples from each candidate source. Use the same finished-product requirement and measurement method; document the preparation each lot actually needs. If different settings are needed to achieve the same accepted powder, record that difference rather than claiming the trials were identical.
- Identify the source, species or controlled blend, bark and contamination history.
- Measure received condition and the prepared feed actually entering the mill.
- Record necessary preparation, removed fractions and relevant energy or handling costs.
- Measure accepted-product mass, particle results and finished moisture on the same basis.
- Record interruptions, return streams and any practical feeding limitations.
- Have the receiving application confirm suitability where size alone is insufficient.
Agree quantities, sampling and test scope through the grinding-test preparation process. This is a proposed comparison framework, not a claim that Tianyuan has already tested the customer’s chips or sawdust.
Apply the Tianyuan model boundary, then choose the feed
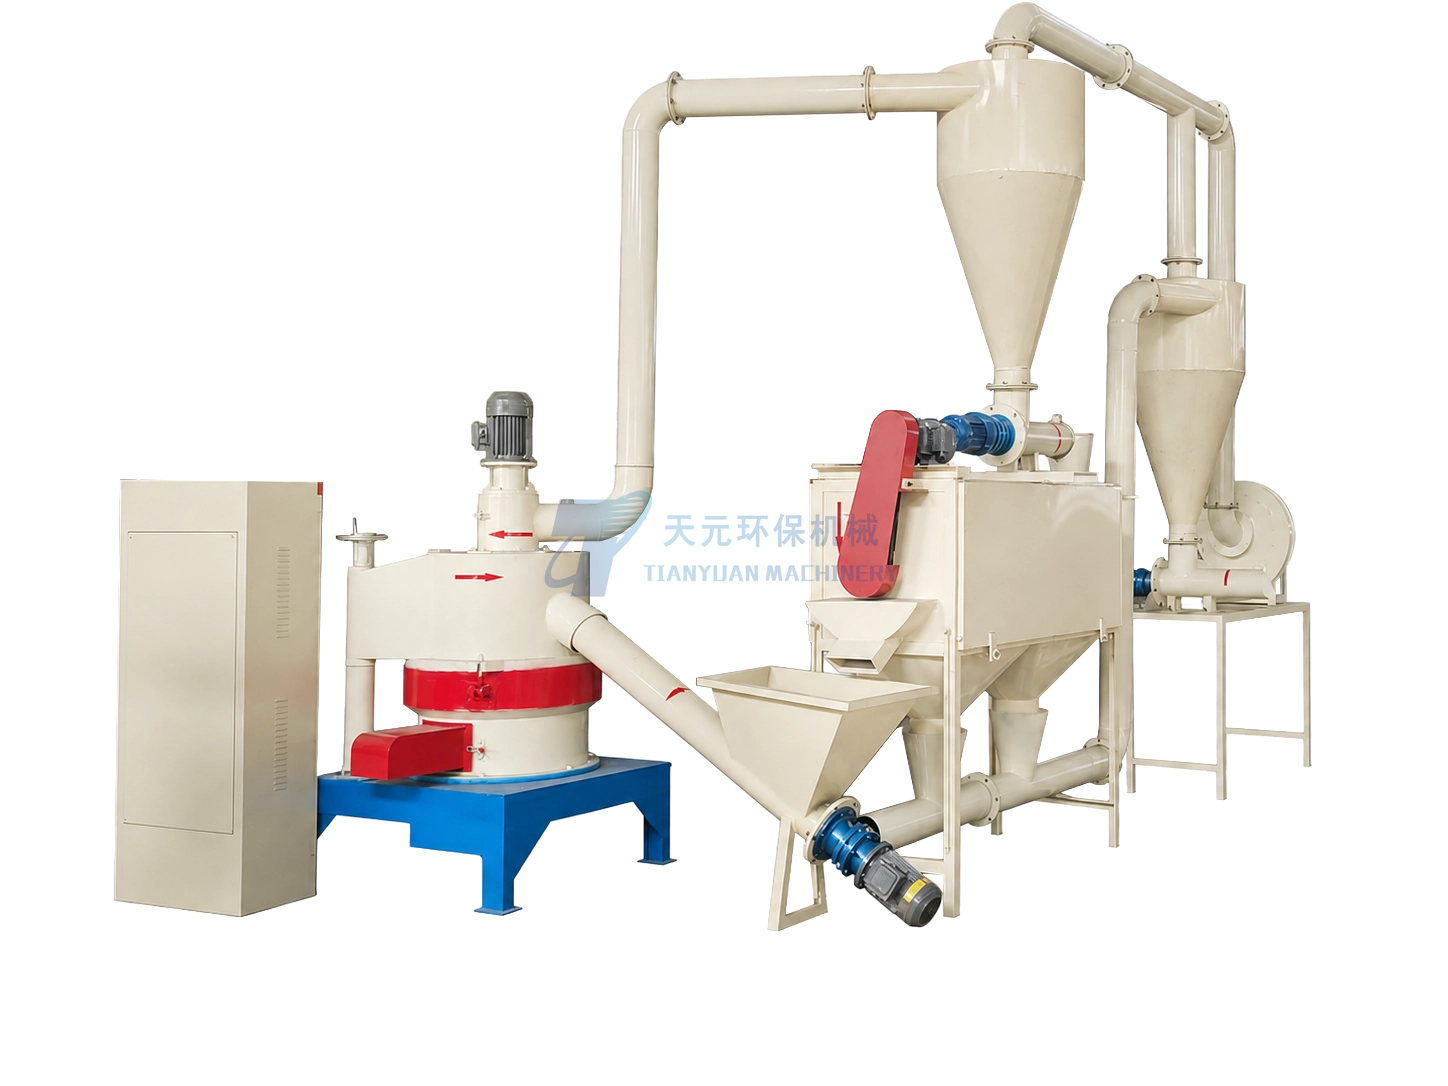
For the TYMF6R-600, the confirmed figures are 30–325 mesh, 100–500 kg/h and maximum feed diameter ≤5 mm. The machine performs downstream fine grinding on prepared woody or plant-fibre materials. Actual capacity depends on material, feed condition, target fineness and site conditions; the range does not guarantee the upper output at the finest setting.
These figures are not universal dimensions for purchased wood chips and do not authorize long strands simply because their diameter is small. Confirm actual form and the manufacturer’s feed conditions for the chosen model; other wood mills have their own specifications.
Contain dust where either feed is transferred and processed; HSE’s wood-dust guidance addresses capture before dispersion. Small particle size is not a safety certificate. Ordinary dust collection or grounding does not replace project-specific fire and explosion protection.
FAQ
Is sawdust always the better feed for wood flour?
No. It can simplify preparation when it is clean, consistent and within the mill’s feed requirements. Poorly controlled sawdust can be less suitable than traceable chips.
Can wood chips be fed directly to the fine mill?
Only when their actual dimensions, shape and condition meet that model’s requirements. Oversized chips need upstream preparation.
Does sawdust always avoid drying?
No. Its moisture depends on its origin, handling and storage. Confirm the actual lot and the required feed and product conditions.
Can two lots with the same mesh target be mixed freely?
Not automatically. Species, contamination, moisture, particle shape and downstream use can differ. Qualify the blend and maintain traceability.
Which cost should be compared?
Use the same stated processing boundary and accepted-product dry mass, rather than purchase price per wet tonne alone. Include only costs that are relevant and avoid double counting.
Conclusion
Select chips or sawdust from evidence about the delivered lot and the required wood flour. Suitable sawdust may shorten preparation; controlled chips may give better raw-material consistency. Compare both at the same approved mill-entry condition and accepted-product target, then decide using verified yield, full process cost and supply reliability.